Yongjian Machinery3 min read
Why two identical tube mills produce very different output
Same machine, same tooling, same material — and one factory produces 40% more saleable tube than the other. Here is where the difference actually comes from.
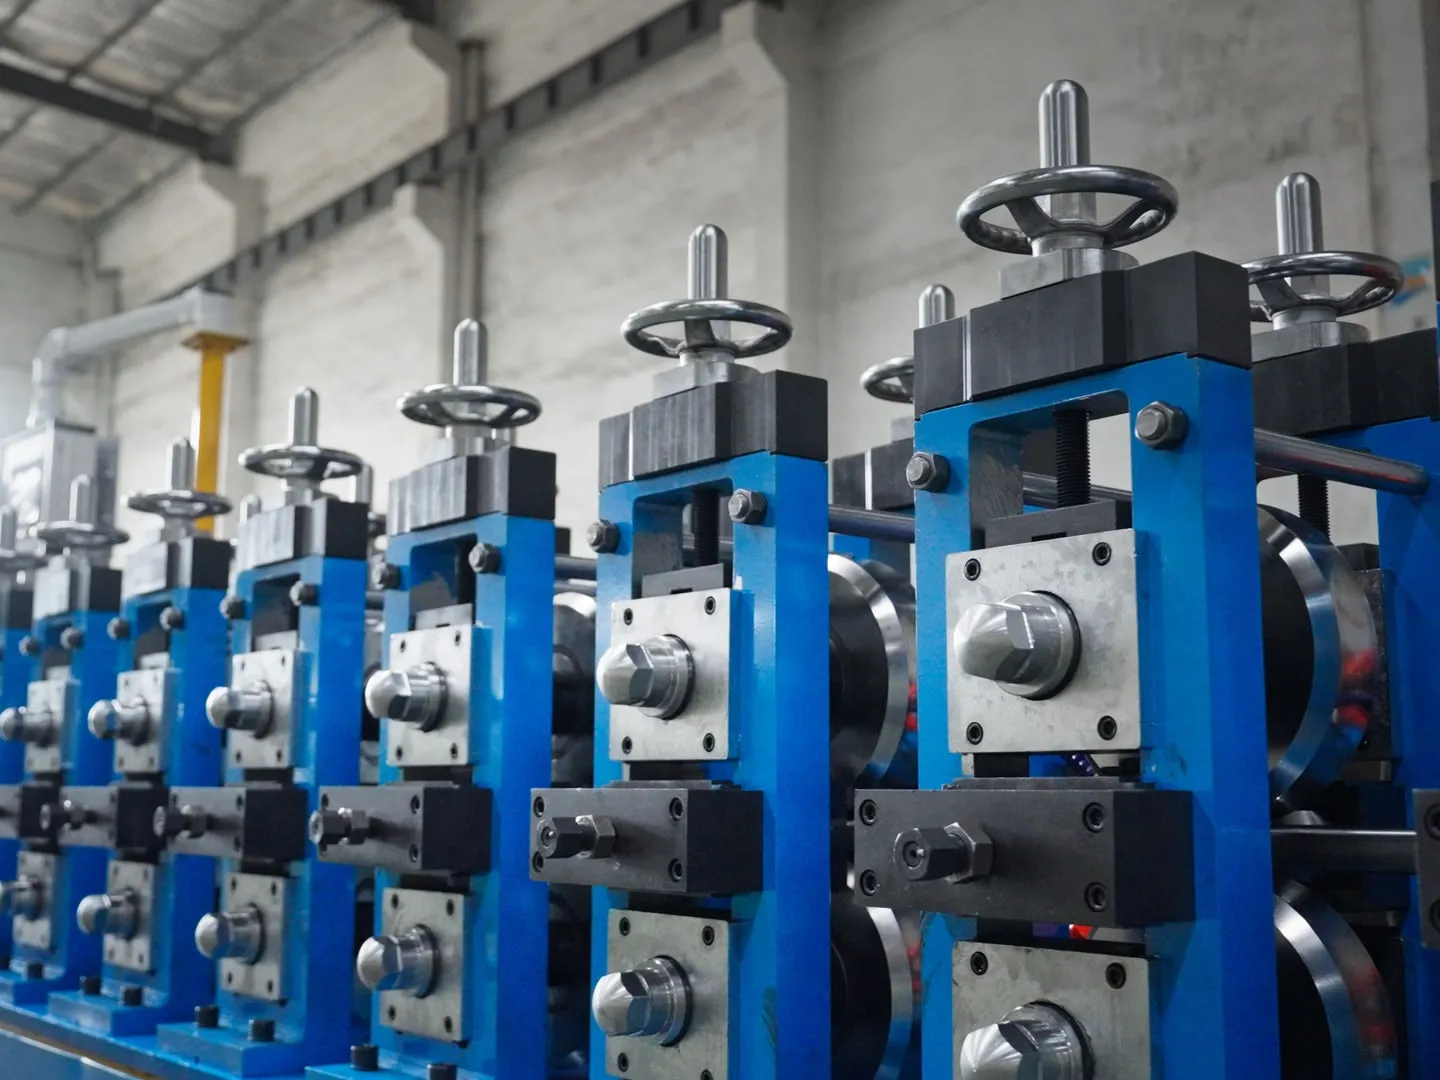
Buyers who have invested in stainless tube production ask us a version of this question constantly: we bought the same equipment and the same tooling as a competitor, so why is their output higher and their scrap rate lower?
It is rarely the machine. Over twenty-five years of commissioning mills we have found the gap almost always comes from five places.
1. Setup discipline
A mill set up correctly for a size — with the settings recorded, and recalled on the next run of that size — produces more and scraps less than one an operator rebuilds from memory at every changeover.
The factories that run well write setups down. Stand positions, weld power, line speed, saw timing. On machines with recipe storage in the control system, this happens automatically. On machines without it, a notebook works nearly as well. What does not work is relying on the operator who has been there longest.
The hidden cost is that an undocumented setup walks out of the door when that operator leaves.
2. Tooling condition
Worn rolls do not stop a mill. They make it produce tube that is slightly out of tolerance, so operators compensate by slowing the line. Output falls gradually and nobody connects it to the tooling, because the machine never actually failed.
Replace roll tooling on condition, measured against a standard — not when it finally produces visibly bad tube. The factories with the best output figures inspect rolls on a schedule and keep a replacement set for their highest-running sizes.
3. Strip quality
Variation in strip width, thickness or edge condition translates directly into weld and dimensional problems. A batch of cheap strip with inconsistent edge condition will cost more in scrap and lost line time than it saved on purchase.
This is the most common false economy in the industry. If your scrap rate moves and nothing about your process changed, check the strip before you check the machine.
4. Weld parameter confidence
Operators who are not sure of their weld settings run below the machine’s capability because the margin feels safer. That margin is pure lost output, and it can be substantial — we have seen lines running at 60% of their rated speed for no reason other than the operator having been burned once by a bad seam.
Fixing this is training, not hardware. Operators need to understand what the weld parameters do, how to recognise a good seam, and how to correct a bad one — so they can run at the machine’s real capability instead of a guessed safety margin.
5. Changeover time
For shops running many sizes in small batches, changeover is the real constraint on monthly output. Not line speed.
Work out how many hours a month your mill spends being changed over versus running. If changeover is a significant share, improvements there are worth far more than a faster line — quick-change cassettes, pre-staged tooling, documented setups, and the discipline to group similar sizes in the schedule.
What this means when you are buying
Four of these five have nothing to do with which machine you buy. They are process and training issues.
That is why our commissioning engineers stay on site until the line is producing tube to specification with your operators running it, rather than leaving when the machine powers up. The handover of process knowledge is the part that determines whether you end up on the high-output side of this comparison.
- Production
- Efficiency
- Operations